

A boiler condensate trap is the water-sealed component at the base of a condensing appliance. It collects acidic condensate from the heat exchanger sump and routes it into the condensate discharge pipe. Its second job matters more than its first: the water seal blocks products of combustion from travelling out of the appliance along the drain line. Lose that seal and you have a combustion product escape path, not just a drainage fault.
For anyone working towards a gas qualification, this is one of the components where the theory and the site reality diverge fastest. Plenty of no-heat callouts logged as “boiler fault” are a trap full of sediment or a discharge pipe frozen solid at the first bend. Knowing the difference saves diagnostic time and prevents the wrong part being fitted.
What does a boiler condensate trap actually do?
It performs three functions at once: it collects, it seals, and it meters the discharge.
A condensing boiler recovers latent heat by cooling flue gases below their dew point, and the water vapour that drops out collects in the sump beneath the heat exchanger. An efficient condensing boiler generates around 2 litres of condensate an hour at roughly 30°C to 40°C, and this needs to be piped to the waste water system or a drain. That volume is not trivial across a heating season, and it has nowhere to go if the trap is obstructed.
The condensate itself is mildly acidic, commonly cited in the region of pH 3 to 4. That is why discharge pipework is plastic rather than metal, and why corrosion staining on brickwork, render or paving below a discharge point is worth flagging on a service sheet.
U-bend traps versus siphon traps
Two designs dominate UK appliances:
- Simple U-bend. Holds a static water seal and drains as a slow trickle.
- Auto-siphon. Fills to a set level, then dumps its contents in a batch.
Whichever design is fitted, boilers must never be run with the trap empty. The seal is what stops combustion gases passing out of the boiler along the condensate drain pipe. If the trap is removed for cleaning, it must always be refilled with water before the boiler is fired again.
The siphon design exists largely as a freezing countermeasure. A batch discharge of warm condensate travels through the pipe with more velocity and less dwell time than a trickle, so it is less likely to freeze in an exposed run. That is also why fitting an additional external U-bend downstream of a siphonic appliance is usually counterproductive.
Where the trap sits in UK regulation
Nothing about condensate work is optional or improvised. Three sources govern it, and they stack in a specific order.
Manufacturer instructions come first. HHIC is clear that the appliance manufacturer’s instructions take precedence over the standard, and following them protects both correct operation and the validity of any warranty.
The relevant British Standard is BS 6798:2014, the specification for selection, installation, inspection, commissioning, servicing and maintenance of gas-fired boilers of rated input not exceeding 70 kW net. It states that wherever possible the condensate drainage pipe shall be terminated at an internal foul water discharge point.
Building Regulations set the drainage outcome. In England and Wales, condensate drainage falls within the wider requirements for sanitary pipework and drainage, particularly Approved Document H, and the legal position varies between England, Wales, Scotland and Northern Ireland. Scotland works to the Technical Handbooks and Northern Ireland to its own Technical Booklets, so check the requirement and the notification route for the nation you are working in.
Above all of it sits registration. Work on gas appliances in Great Britain must be carried out by a Gas Safe registered engineer where registration is required. The trap is part of the sealed combustion circuit on a room-sealed appliance, so removing, cleaning and refitting it is gas work, not plumbing.
Signs of a blocked boiler condensate trap
Sediment is the usual culprit. Corrosion products and debris from the heat exchanger and sump settle over years of operation, and eventually the flow path closes. If enough sediment builds up, it stops the flow of condensate, the liquid backs up into the bottom of the heat exchanger, and the boiler shuts down for safety.
Look for the following on site:
- A condensate-specific lockout or fault code. Codes are manufacturer specific, so read the code against the appliance manual rather than from memory.
- Gurgling or bubbling from inside the appliance as condensate backs up.
- The boiler firing and then cutting out a short time later, repeatedly.
- Water inside the case, overflow from the sump area, or drips from the underside of the appliance.
- The boiler shutting down while the external discharge pipe is visibly clear, which points at the trap rather than the pipe run.
- Dark, carbon-like deposits in the trap body on removal, which indicate the blockage has been building for a long time.
Where the trap body is clear plastic on some models, the collected condensate is visible inside, which speeds up the initial check.
Working out whether it is the trap, the pipe or the drain
Three separate faults present almost identically, so work through them in order rather than going straight for the trap.
Start outside
A frozen condensate pipe is the most common cause of boiler breakdowns in cold weather, and the external section is the part most exposed below zero. Thaw with warm water, not boiling water, and never with a naked flame.
Then check the termination
A blocked gully, a silted soakaway, or a waste connection altered during a kitchen refit will back the system up just as effectively as a blocked trap.
Then check the pipe run
Horizontal sags, insufficient fall, undersized pipe and reduced bores at push-fit fittings all cause pooling and eventual blockage. For reference, BS 6798 sets a minimum fall of 45mm per metre away from the boiler, with 52mm per metre commonly used as industry practice. Expressing fall as “3 degrees” only applies to the short section passing through the wall on an external run, so do not carry that figure across the whole pipe.
Only then remove the trap
If it comes out clean and the appliance still faults, the restriction is likely to be the sump spigot or the drain hole between the heat exchanger and the trap, which can silt up independently.
How to service a boiler condensate trap safely
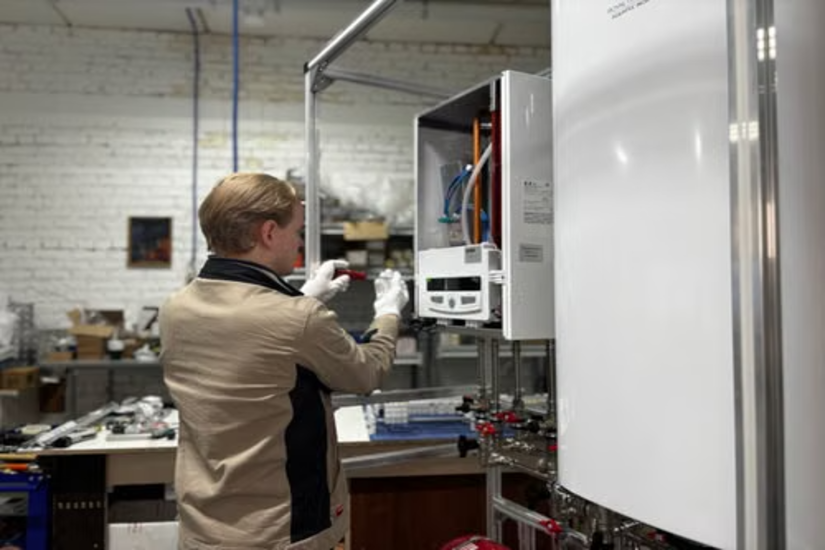
Cleaning is a routine part of an annual service and should follow the manufacturer’s published procedure. The sequence below reflects standard practice, but the manufacturer’s instructions override it in every case.
- Isolate. Turn off the gas and electrical supply and allow the appliance to cool.
- Protect the area. Condensate is acidic and will mark flooring and worktops.
- Remove the trap as described in the appliance instructions, retaining any washer, O-ring or clip.
- Empty and flush the trap with clean water until the flow path is clear. Do not use aggressive chemicals or boiling water on plastic components.
- Inspect the sump outlet and the drain hole feeding the trap, since a clear trap on a blocked spigot is a wasted visit.
- Check the seal. A perished, missing or misplaced washer will break the water seal and, on siphonic designs, stop the siphon working altogether.
- Refill the trap with clean water before refitting. This is not optional.
- Refit and reseal the case correctly, then recommission and carry out a combustion check, including flue gas analysis, exactly as the manufacturer specifies. Disturbing the sealed circuit is precisely when that check matters.
- Record the trap check on the service documentation.
HHIC advises that remedial or servicing work should include a condensate discharge pipe check, with any action required explained to the customer.
Maintenance risks worth taking seriously
- Running the appliance with a dry trap. This is the risk that outranks all the others. An empty trap leaves an open route for products of combustion into the property. Diverting the condensate outlet into a bucket as a temporary measure creates exactly this condition and should never be used as a workaround.
- Incorrect refitting. A trap refitted without its seal, or not fully seated, can allow flue products to escape. If flue products can enter the premises, the installation must be classified and actioned in line with the current Gas Industry Unsafe Situations Procedure.
- Treating the symptom instead of the cause. Heavy carbon or corrosion deposits point somewhere else, usually combustion performance or heat exchanger condition. Clean the trap, then find out why it filled.
- Modifying components. Drilling out a restriction, cutting down a trap body or substituting a non-approved part changes the appliance from its certified condition and invalidates the warranty.
- Ignoring the pipework while focusing on the appliance. A trap cleaned every year on a pipe run that freezes every January solves nothing.
Getting the condensate discharge pipe right
Most repeat callouts trace back to the install. HHIC’s installer guidance sets out the practice that avoids them.
Terminate internally wherever it is achievable. Where an external run is the only option, the pipe should be increased to a minimum of 30mm internal diameter (typically 32mm outside diameter) before it passes through the wall. Through the wall it should slope downwards by at least 3 degrees to keep a good velocity as the condensate exits, and the external run should be kept as short as possible, up to a maximum of 3 metres, taking the most direct and most vertical route with no horizontal sections in which condensate might collect.
For insulation, use lagging rated for outdoor life: a minimum of 13mm thickness that is both waterproof and UV resistant, not internal foam. Consider trace heating on exposed runs in high wind chill locations.
Where a visible air break is specified at a soil stack connection, note that it is not required if a trap with a minimum condensate seal of 75mm is incorporated within the boiler. Confirm the requirement in the appliance instructions before deciding.
Do not discharge into a rainwater downpipe unless that downpipe feeds a combined foul and rainwater system, and even then an external air break must be fitted to prevent reverse flow. Surface water drainage is not intended to receive boiler condensate, and older properties may have separate drainage systems. Where a foul connection is genuinely impractical, a purpose-made condensate soakaway installed to the manufacturer’s instructions and current drainage guidance is the recognised alternative.
A note on condensate neutralisers
Where a neutraliser is fitted to raise the pH of the discharge, it sits downstream of the trap, never before it. Placed ahead of the trap it would offer a bypass route around the heat exchanger for flue gases, which is exactly what the water seal exists to prevent.
For anyone still getting familiar with boiler servicing, condensate systems, and common fault checks, TradeFox gives you a practical way to keep learning between jobs. You can revisit gas engineering simulations at your own pace and reinforce the steps before carrying them out in supervised training.
Take the detail seriously and the callbacks stop
The condensate trap is a low-cost component with high consequences when it is handled casually. Clean it properly, refill it every time, inspect the pipework that feeds and leaves it, and record what you found. Engineers building a reputation for first-visit fixes tend to be the ones checking the whole condensate route rather than the part that is easiest to reach.